Subscribe to Blog
Email Address
 
Search for cnc returned 15 results.

A Total Guide into Plunging and Ramping

April 5, 2017, 12:33 am by Eldar Gerfanov (Admin)

Before we start milling away our stock we first need to get down to the required depth.

This is not a problem with external features when we can plunge outside.

When machining closed pockets, however, we need to find a way to get down to the machining depth first.

As usual there are several ways to get the job done. The plunging methods listed here are not ordered by their preference.

For various machining operations on different materials some may be more preferable than others.

Straight Plunging into a larger Pre-Drilled hole
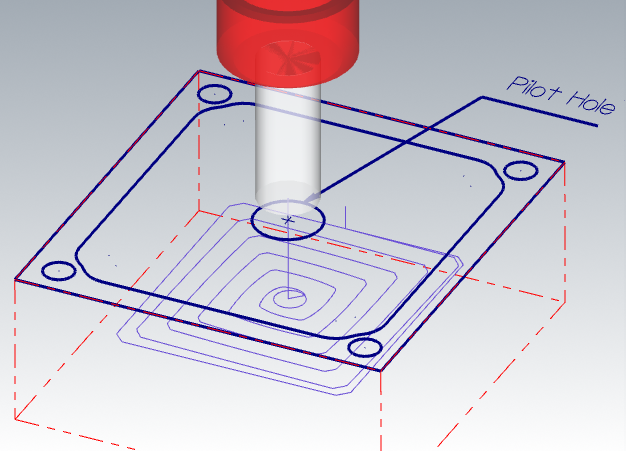
This is one the best ones in my opinion.
Very few machining modes can compete in effectiveness with drilling and this method will get you the best combined tool life on most materials and (in case of many deep pockets) the least machining time, even when tool change time is factored in.
Read More 
Tool_Length_Offset.PNG

Did you know there are three ways you can touch off your tools?

Because of how Machine Offsets add up, there are several ways CNC machinists can set their Tool and Work Offsets.

This is especially true for Tool Length Offsets.

Tool Offsets can be either Positive or Negative.
Depending on your Machine Shop equipment you should use one or the other.

Regardless of how you set your tool length offset, you apply it the same way.
Right after the tool change and after turning on your spindle and moving to your X Y position above the part.
The very first absolute Z movement should be the line where you apply the tool length offset.

Code
T15 M6; (TOOL CHANGE)
G0 G54 G90 X1.0 Y1.5 S1500 M3;(APPLY WORK OFFSET, MOVE TO THE FIRST POSITION, TURN ON THE SPINDLE)
G43 Z2.0 H15; (APPLY TOOL LENGTH OFFSET WHILE MOVING TO 2.0" ABOVE THE PART)
G0 Z0.1 M08;(MOVE TO FEED HEIGHT AND CARRY ON WITH THE PROGRAM..)

Positive Tool Offsets (gage line tool length offsets)

In the case of Positive Tool Offsets, the offset represents the Length of the tool measured as a distance from the Gauge Line of the spindle (typically spindle nose) to the tip of the tool. The longer the tool, the larger your Tool Length offset will be.

Read More 

And this is why you have safety doors on cnc lathes.....

August 31, 2013, 9:07 pm by Eldar Gerfanov (Admin)

.....and this is why they are so heavy.

I have stumbled upon this video the other day.

It shows a very good reason to keep those doors closed at all times when runing your machine.

Pictures of Nested Parts

December 9, 2012, 10:10 pm by Eldar Gerfanov (Admin)

Here are some samples of nested parts i did recently

In both cases back of all pieces were machined at the same time, dowel holes milled so that there would be a way to align top and bottom.

Ealot of material was lost, but it was a scrap anyways, so all i gained was alot of saved man-hours.

Photobucket

And here are 4 more pictures:

Read More 

Repeating OKUMA CNC Lathe program number of times

January 6, 2011, 6:00 pm by Eldar Gerfanov (Admin)

If you want OKUMA Lathe to repeat program several times you can use a subprogram or a conditional GOTO statement.

On Many Okumas subprograms is an option you have to buy, so we have to use GOTO statement.

Code
O1 
CN=7 (NUMBER OF CYCLES TO REPEAT) 
CC=0 (CURRENT CYCLE)
N0
......
(part program)
......
CC=CC+1 
IF [ CC LT CN ] N0 
M2

Thats it 

This little code helps alot when using bar feeder and stuff like that.


Sing In

© 2009-2022 Eldar Gerfanov. All Rights Reserved.
© 2009 Eldar Gerfanov. Materials on this site are presented as is and are mostly for educational use.

You may freely reproduce information presented herein without any consent from me, provided you include link to this site.
In case when i am not the copyright holder, you may want to contact proper owner of material. Anyway, they are freely available on the Internet.
If you hold the copyright right for any of the materials on this site and want them removed, please contact me here